Boiler Hydraulic Test in Bangladesh
A boiler hydraulic test in Bangladesh is a pressure test in which the boiler is completely filled with water and pressurised above its working pressure, then held while an inspector checks every seam, tube, joint and fitting. It proves the pressure parts are tight and sound, and it is part of the inspection behind registration and certificate renewal under the Boilers Act 1923.
A boiler hydraulic test in Bangladesh is one of the most important checks a factory can make on its steam plant. Boilers in garment washing, dyeing, food, pharmaceutical and textile plants operate every day under pressure and temperature, and the pressure parts slowly lose thickness through corrosion, scale and erosion. TOTO POWER Engineering, an engineering consultancy operating since 2011 and enlisted with the Department of Inspection for Factories and Establishments (DIFE), helps plant owners prepare for, carry out and document hydraulic tests on boilers and other pressure equipment from our Dhaka and Chittagong offices.
What is a boiler hydraulic test?
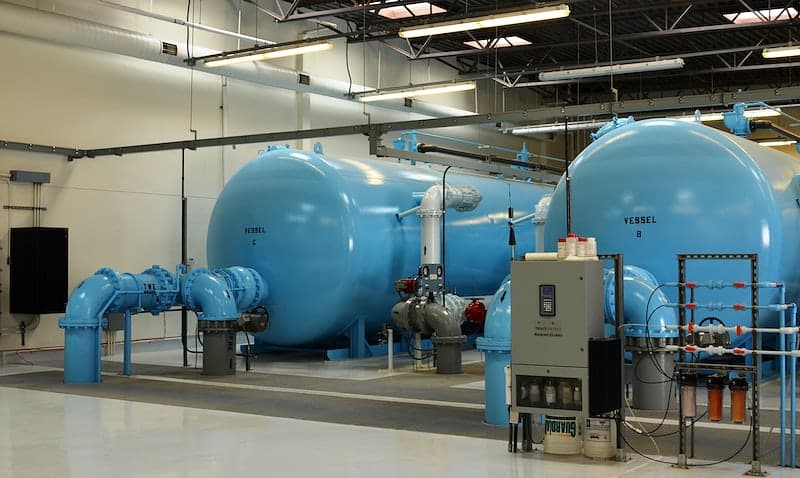
A hydraulic test (also called a hydrostatic test) checks the strength and tightness of a boiler's pressure parts. The boiler is isolated, completely filled with water, vented so that no air pockets remain, and then pressurised with a hand or motorised test pump to a pressure higher than the pressure it is allowed to work at. That pressure is held for a set period while the inspector examines the shell, end plates, furnace, tubes, tube plates, stays, welded seams, manholes, mudholes and every mounting connection for leaks, weeping, bulging or other distortion.
Because the boiler is cold and filled with water, the test reveals defects without the risk of a steam release. A leak shows up as a drop on the calibrated pressure gauge and as water at the defect, so it can be found and repaired before the boiler is fired again.
What is the purpose of a boiler hydraulic test?
- Prove tightness: confirm that seams, tube expansions, gaskets and fittings do not leak at a pressure above normal operation.
- Prove strength: show that the pressure parts can carry the test load without permanent deformation, which would indicate thinning or a design or repair problem.
- Verify repairs: check that welding, re-tubing or plate repairs are sound before the boiler goes back into service.
- Support certification: give the inspecting authority, insurers and export buyers objective evidence that the boiler is safe to operate.
Which law applies: the Boilers Act 1923
In Bangladesh, steam boilers are regulated under the Boilers Act 1923 and the regulations made under it. The Act is administered by the Office of the Chief Inspector of Boilers. In general terms, a boiler must be registered before it is first used, and the owner must hold a valid certificate authorising its use at a stated maximum pressure. Certificates are issued for a limited period and must be renewed; renewal follows an inspection by a boiler inspector, and that inspection normally includes an internal examination and a hydraulic test. A boiler that has had a major repair or alteration, or has been moved, is also expected to be re-examined before use.
The exact certificate period, the fees, the forms and the scheduling of the statutory inspection are set by the Chief Inspector's office and can change, so plant owners should always confirm the current requirements directly with that office. Our role is to prepare the boiler and the documents, carry out independent pre-tests, attend the test, and give you an engineering record you can use for factory compliance, insurance and buyer audits. Boiler safety also forms part of a wider safety assessment of a factory.
Who needs a boiler hydraulic test?
- Factories renewing a boiler certificate or registering a new or relocated boiler.
- Plants that have repaired, re-tubed or modified a boiler.
- RMG washing and dyeing units preparing for a buyer or insurer safety audit.
- Owners buying or selling a used boiler who need evidence of its condition.
- Plants where a boiler has been idle for a long time and is about to be restarted.
How is the test pressure decided?
The test pressure is always set above the boiler's approved maximum working pressure, so that the test proves a margin of safety. A value of about 1.5 times the maximum working pressure is commonly specified for hydraulic tests, but the correct figure for a particular boiler depends on its design code, its age and condition, any repairs made, and the instructions of the inspecting authority. An older boiler may be approved for a lower working pressure than its original rating, and the test pressure follows that approved value. We never choose the test pressure by habit: we confirm it in writing from the boiler's documents and the authority's requirements before pressurising.
How do you prepare a boiler for a hydraulic test?
- Shut down and cool: take the boiler off line and let it cool naturally. Never force-cool with cold water.
- Isolate: close and lock the steam stop valve, feed valve and blowdown valves, isolate the fuel and electrical supply, and fit blank flanges where a valve alone cannot be relied on.
- Drain, open and clean: drain the water, open manholes and mudholes, and remove scale and sludge so that the internal surfaces can be examined.
- Internal inspection: look for corrosion, pitting, cracks, bulges, leaking tube ends and damaged stays before the test, and record what is found.
- Protect fittings: remove or gag the safety valves as instructed, so they are not damaged and do not lift during the test, and fit a calibrated test gauge.
- Documents ready: keep the registration documents, the previous certificate, drawings and repair records available for the inspector.
How is a boiler hydraulic test carried out?
- Fill and vent: fill the boiler completely with clean water at ambient temperature, opening the vents at the highest points until water runs out without air.
- Raise pressure gradually: pump the pressure up in stages, pausing to check for leaks, until the working pressure is reached.
- Reach test pressure: continue slowly to the agreed test pressure, watching the calibrated gauge. Nobody stands in front of blanks, plugs or gauge connections while the pressure rises.
- Hold: isolate the pump and hold the test pressure for the specified period, noting any drop on the gauge.
- Examine: reduce to a lower pressure if the procedure requires it, then examine all seams, tube ends, stays, mountings and joints closely for leaks, weeping and distortion.
- Release and drain: release the pressure slowly, drain the boiler, re-inspect any suspect areas and restore the safety valves and fittings.
- Record: note the test pressure, hold time, gauge identification, observations and result, with photographs.
What are the acceptance criteria?
A boiler passes a hydraulic test when it holds the test pressure for the specified period without a significant pressure drop, shows no leakage or weeping from seams, tube ends, stays or fittings, and shows no visible permanent deformation such as bulging of the furnace, shell or end plates. Any leak, drop or distortion is a failure: the cause is investigated, the defect is repaired by a competent boiler repairer, and the boiler is tested again.
| Observation during the test | What it usually means | Next step |
|---|---|---|
| Pressure holds, no leaks, no distortion | Pressure parts are tight and sound at test pressure | Pass; record and restore the boiler |
| Weeping at a tube end or gasket | Loose tube expansion or poor gasket seating | Re-expand or re-seat, then retest |
| Leak from a weld or plate | Crack, porosity or thinning | Further examination and approved repair, then retest |
| Bulging or permanent set | Overheating damage or loss of thickness | Stop; engineering assessment before any decision |
What safety precautions are taken?
- Water only, at ambient temperature; air is vented completely before pressurising.
- Calibrated pressure gauges, with a second gauge as a cross-check where possible.
- Pressure raised gradually, never beyond the agreed test pressure.
- The test area is barricaded, and only essential people are present.
- Fuel, steam and electrical isolation with lock-out and tags throughout the test.
- No hammering, welding or tightening on parts while they are under pressure.
- Confined space precautions for anyone entering the boiler for internal inspection.
What you receive
- A pre-test checklist and the confirmed test pressure, with its basis.
- A hydraulic test report: boiler details, test pressure, hold time, gauge details and result.
- Internal and external inspection findings, with photographs of any defects.
- Repair recommendations and a retest record where repairs were needed.
- Supporting records to help with the certificate renewal file, insurance and buyer audits.
Related pressure tests
Air receivers and compressed air tanks are unfired pressure vessels that need the same careful approach. See our hydraulic pressure testing of air receivers service. For a full list of our tests, visit the testing and inspection services page.
What does a boiler hydraulic test cost in Bangladesh?
The cost depends on the boiler type (fire-tube or water-tube), its size and pressure, how much cleaning and blanking is needed, whether internal inspection and thickness checks are included, the site location and whether repairs and a retest are required. Statutory fees payable to the Chief Inspector of Boilers are separate. We visit or review the boiler details first and then send a written quotation.
Why choose TOTO POWER Engineering?
We have worked with industrial clients, especially in the RMG sector, since 2011 and have completed more than 500 projects. Our engineers prepare the boiler properly, test with calibrated instruments, follow a written procedure, and report clearly, so the result is useful for compliance as well as for maintenance planning. Because we also carry out electrical, fire and structural assessments, we can look at the whole boiler house rather than the boiler alone.